
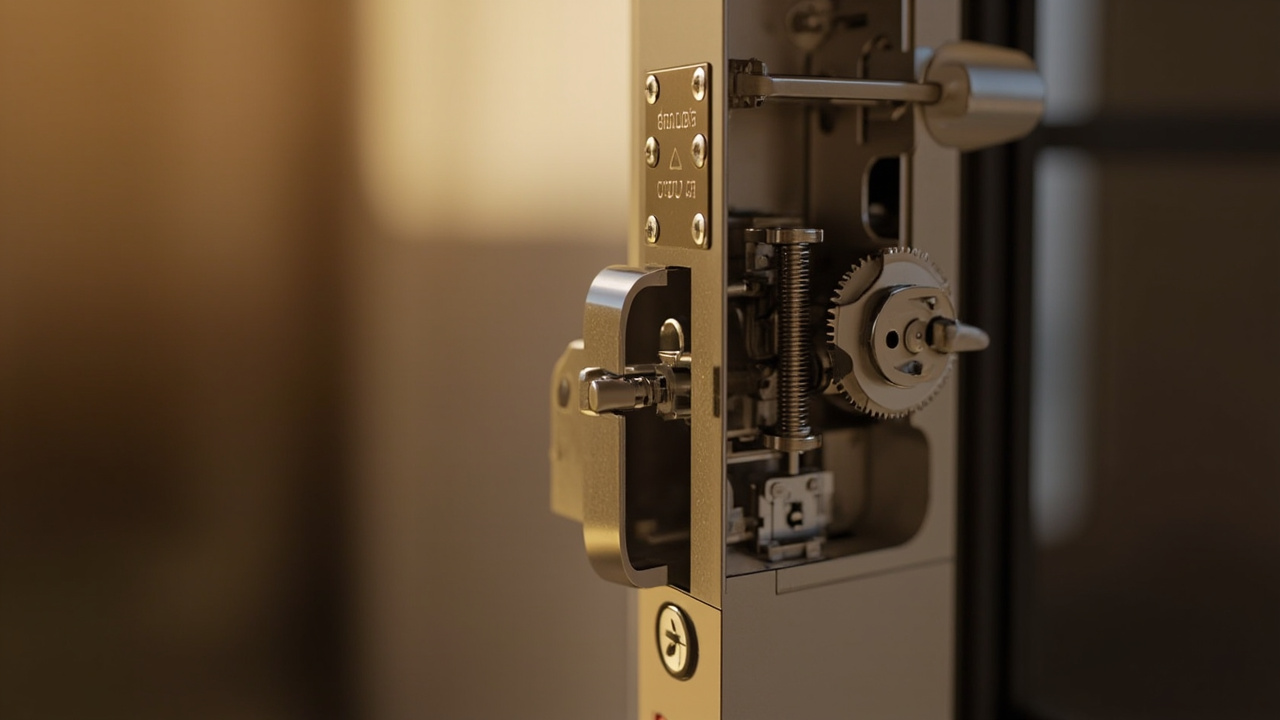
Surface Finish Processes Trade-Offs: Cost, Durability and Service
Technology claims are cheap and verification is not, so surface finish processes tradeoffs is treated here as a set of checks. Cross-Border Diary — qualification notebook for a system integrator
Direct answer. In brief, this article covers surface finish processes tradeoffs from surface finish processes tradeoffs to surface-finish-processes. It states what to confirm about surface finish processes tradeoffs on the dated product page where a figure is involved. A surface finish processes tradeoffs is a component behaviour guide. It covers limits. It covers failure modes. surface finish processes tradeoffs decides whether surface finish processes tradeoffs is acceptable for this build.
Read surface finish processes tradeoffs as surface finish processes tradeoffs. It is a working definition of surface finish processes tradeoffs. Not a statutory or certified one. It applies to the market and product in question rather than as a general claim.
- Establish the reach — confirm on the dated product page for the specific SKU behind surface finish processes tradeoffs
- Establish the edge — record where the technology in surface-finish-processes stops working
- Establish the reserve — name the mechanical path that remains if surface finish processes tradeoffs fails
- This is the sequence surface finish processes tradeoffs has to follow, anchored on surface finish processes.
This is a composite Cross-Border Diary for a system integrator qualifying smart lock finishes across a factory-to-project handoff. It is not a customer case study and makes no claim about a visit to a named supplier. The entries show how a sample, a process description, and a service obligation can separate in transit. The recurring issue was simple: surface finish processes tradeoffs were discussed as if color were the only output, while the real purchase also carried edge wear, hidden-part protection, matched replacement, and technician time.
I use composite here deliberately. It keeps the diary useful without inventing a client, a shipment, or a supplier result. Every technical recommendation below is framed as a question, an inspection point, or a document to request. The only first-party product reference is the verified catalogue anchor noted later. This format reflects the system integrator’s qualification stage: define evidence and release conditions before commercial approval.
The border was also a sample-control point
The first entry concerns control rather than coating. A finish sample can leave the factory approved, cross an ocean, and arrive without the contextual information needed to judge it. Different lighting can alter perceived color, a protective film can leave an adhesive mark, and one packed sample may not represent every production configuration. Without a shared identifier, the receiving team cannot connect the physical sample to the drawing, process route, and approval request.
At the receiving desk, I would ask for a sample record rather than a decorative photograph. The record needs the exact part, finish designation, substrate, process route, visible side, masking instruction, and any coating or surface-treatment limits. It should also identify which sample is the approval master and which are working pieces for installation, handling, or service evaluation.
The survey work has to follow the same discipline. An Office Smart Lock Site Survey may establish traffic and hardware conditions, while a Smart Lock Retrofit Site Survey exposes the door thickness, frame condition, and retrofit constraints that influence both finish selection and replacement planning. The factory receives the survey result as an input; it is not evidence that a particular finish will suit the door.
Entry one: map what visitors actually touch
Before asking which process looks best, I divide the lock into visible, contact, concealed, and moving families. The escutcheon, handle or lever, keypad, fingerprint sensor, RFID reader, cylinder collar or rose, and emergency power port are immediately visible or touched. The lock body, mortise case, latch, deadbolt, strike plate, strike keeper, spindle, and motor-driven components mostly live inside the door or its frame.
That distinction changes the acceptance question. A visitor may reject an inconsistent panel color while never seeing the lock case. A technician may replace a damaged strike plate whose visual finish matters less than its edge condition and fit. Fingerwear on the keypad or fingerprints around the sensor create another service concern that cannot be assessed from a coated display panel alone.
The catalogue offers a useful but narrow first-party anchor. The SLK-9936S hotel lock is listed with a stainless steel + alloy body and multiple finish options. That line does not assign a process to each part; confirm on the dated product page for the specific SKU before using it in a procurement decision.
flowchart TD
    A[Separate visible and hidden parts] --> B[Map substrate and geometry]
    B --> C[Compare process routes]
    C --> D[Inspect wear and edge conditions]
    D --> E[Build cost and service record]
    E --> F{Evidence complete}
    F -->|Yes| G[Approve controlled sample]
    F -->|No| H[Hold release and request evidence]
A surface finish process comparison is only meaningful when the part and acceptance condition are fixed. This working map treats each route as a hypothesis that the supplier and buyer must test against their own drawings and use case.
| Finish route | What the route changes | Main qualification trade-off | Likely service question |
|---|---|---|---|
| PVD | Deposits a thin film on a prepared base | Color and appearance depend on the base, preparation, and process controls | Will edge damage expose the base, and can a replacement panel be matched closely? |
| Electroplating | Builds a metallic layer by electrodeposition | Pretreatment, coverage, and consistency need review by part geometry | Can a damaged area be restored without replacing the whole visible component? |
| Powder coating | Applies a polymer layer that is subsequently cured | Film build, texture, and cure affect appearance and edge behavior | Will chipping remain cosmetic, and what local repair method is permitted? |
| Anodizing | Creates an oxide layer on aluminum | The route is substrate-specific and masking can affect appearance | Is the aluminum part approved for this route, and can a later machining mark be accepted? |
| Passivation or mechanical preparation | Changes surface chemistry or texture without a decorative color layer | It may reduce visual complexity while revealing natural material variation | Is appearance variation acceptable, and how will scratches be distinguished from coating loss? |
No route wins automatically. The correct choice depends on where the part sits, how it is touched, what the service organization can maintain, and how appearance is judged after installation.
Entry two: follow the part through the finish line
Following one component through the process reveals why equivalent-looking samples can carry different cost structures. A panel with a recessed sensor window may need masking. A curved lever may need a different holding method from a flat escutcheon. A strike plate may have sharp edges, while a lock case has pockets and moving interfaces that complicate uniform coverage.
At the commercial desk, I would request the cost logic behind every stage. A useful quote should distinguish process setup, fixtures or racking, pretreatment, masking, coating or deposition, curing where applicable, inspection, rework, protective packing, and matched spare parts. It should also state the assumptions about part geometry, color, volume grouping, and packaging.
A cosmetic finish specification can hide an expensive service decision. For example, demanding a visually exact panel replacement may require retaining a master sample, defining a replacement source, and approving the acceptable color range. A less visible panel might justify a simpler matching standard, but the decision should be recorded rather than assumed.
| Cost pool | Evidence to request | Why it changes the comparison |
|---|---|---|
| Process setup and fixtures | Which steps are dedicated to this part or color route | The same visible result can carry different preparation and handling burdens |
| Masking and selective treatment | Which areas are protected and which are exposed | Selective work can reduce treatment area but add labor and inspection points |
| Inspection and rework | What defect classes trigger rejection or repair | Rework rules affect both quoted cost and delivery confidence |
| Packaging and spares | How samples, replacements, and mixed configurations are identified | A serviceable product can still create cost if matching parts cannot be found |
| Commercial assumptions | The quoted volume grouping, color scope, and exact MOQ for each route | Like-for-like comparison is impossible when each quote covers a different scope |
The exact figures belong in a quote-based review. No useful ranking comes from a generic statement that one process is always cheaper. I would compare the same geometry, color expectation, acceptance limits, packing, and service quantity before deciding whether the commercial difference justifies a process change.
Entry three: put the wear line beside the color chip
The next inspection moves away from a straight-on display. I examine edges, fastener seats, handle roots, keypad boundaries, sensor borders, cylinder interfaces, latch corners, and the visible edge of the strike plate. These are locations where handling, installation, contact, and cleaning can reveal differences that a polished front panel conceals.
The question of smart lock finish durability has to be separated from the question of cosmetic durability. A scratch may leave the lock fully functional while changing its acceptance by the end user. Conversely, a concealed part may look perfect but develop an edge or interface problem before the visible panel shows anything. A finish decision that uses one expectation for every component is not engineering.
At interfaces between different metals, finish selection can become part of the corrosion-control discussion. The interface itself, the preparation route, the fastener material, and the service environment all matter. I would ask the supplier to identify where dissimilar materials meet and what evidence supports the proposed combination, rather than assuming the panel and case were evaluated as a set.
Good finish failure diagnostics begin before failure. The incoming inspection should distinguish coating loss, material transfer, adhesive residue, handling abrasion, installation damage, and ordinary dirt. Each category points to a different owner and corrective action. The detailed Surface Finish Processes Failure Modes Seen on Smart Lock Projects is useful for building that inspection vocabulary without reducing every blemish to the same cosmetic defect.
Entry four: test the service technician’s reality
For lock finish serviceability, I move the sample from the display stand to the installation bench. The test is deliberately ordinary: remove the panel, handle the lock as a technician would, mark the parts that need protection during work, and record which surfaces become damaged by contact with tools, packaging, or adjacent hardware.
That exercise produces a replacement hierarchy. Some damage can be handled by cleaning or replacing a small external component. Some requires a complete visible assembly. A third category involves the lock case or interface, where appearance approval alone is irrelevant because the entire functional component has to move. The hierarchy should appear in the service method, not remain an informal understanding at the distributor.
Finish failure diagnostics then become a service-design input. If scratches are difficult to distinguish from coating loss, the technician needs an agreed reference. If two batches do not match closely, the design may need a controlled spare process. If an exposed edge is vulnerable, assembly instructions may need to identify the handling point. These are operational responses that can be designed before field deployment.
For the wider buyer context, Surface Finish Processes in a Smart Lock: What a Buyer Should Understand explains the component-level view, while Maintenance Implications of Surface Finish Processes Choices extends the discussion into routine upkeep. I would keep both references beside the service procedure because they answer different questions: what is being finished and what happens after handover.
Entry five: turn observations into a qualification file
Before the sample crosses back across the border, the evidence needs a common index. Photographs can identify appearance, but they cannot carry every process variable. The shared record should connect the approved sample to the drawing revision, part number, color reference, substrate, route, masking, acceptance notes, and supplier response.
The Surface Finish Processes Test Evidence a Buyer Can Actually Request is particularly useful for deciding which evidence deserves a place in that file. The objective is not to collect impressive-looking reports. It is to connect each proposed use condition and risk to evidence that speaks to it, then identify any uncovered condition before release.
| File item | Minimum useful content | Approval use |
|---|---|---|
| Approved sample record | Part, route, color reference, visible side, sample identifier, and revision | Stops the physical sample from becoming an uncontrolled reference |
| Part and process map | Which components receive which treatment and which surfaces are masked | Connects appearance decisions to hidden and moving parts |
| Material declaration | Substrate and relevant alloy or surface condition | Allows the proposed route to be checked for suitability |
| Layer or treatment declaration | What the route adds to the surface and where it applies | Prevents a generic finish name from replacing engineering detail |
| Evidence index | Method, specimen, condition, result, date, and scope | Shows which risks were evaluated and which were not |
| Cosmetic acceptance record | Color, gloss, texture, marking, and defect limits as applicable | Gives the receiving team more than “looks acceptable” |
| Traceability and change record | Batch or process control reference and notification method | Creates a route for handling a future process or material change |
| Service matching record | Replacement source, matching standard, and master-sample control | Connects production quality to a workable repair method |
The catalogue can identify available options, but it cannot fill gaps in this file for a particular finish. A translated summary is useful for a cross-border team, but the controlled drawing and approval record must remain identifiable across both languages.
Entry six: compare routes without false precision
There is no universal finish winner for a smart lock. The exterior panel, reader, lock case, strike plate, and cylinder interface may need different priorities. A route that satisfies color consistency across visible panels may still be unattractive for the service organization if replacements cannot be matched. A durable route may be technically suitable but commercially unjustified for a concealed component that has little visual duty.
The decision table below is a starting set of questions, not a generic product ranking. The buyer should replace each hypothesis with project-specific evidence before selecting the route.
| Decision condition | Route to investigate first | Trade-off that must remain visible | Stop or hold condition |
|---|---|---|---|
| Several visible panels must appear consistent | PVD or electroplating with controlled color matching | Thin-film or metallic appearance may vary with base condition and processing | The supplier cannot define the base, route, or matching standard |
| Parts face frequent hand or tool contact | A route with demonstrated edge and wear behavior for that geometry | Added appearance sophistication may increase the cost of a damaged replacement | Evidence covers only a flat coupon, not the relevant part shape |
| Exterior and internal components use mixed metals | The complete assembly and its interface documentation | Process selection cannot be isolated from fastener and substrate compatibility | The proposed route is evaluated without interface information |
| Field replacement must look acceptable | A route supported by controlled spare samples and matching rules | A narrow color range may increase spare inventory or complicate procurement | No responsible matching method is documented |
| Aluminum components require a metallic appearance | Anodizing with the intended masking route | The treatment is substrate-specific and machining can affect the final surface | The drawing permits a substrate or later machining condition that the route cannot accept |
| Polymer-coated parts need broad color or texture choice | Powder coating with the proposed film and cure route | A thicker appearance layer can make edge damage more visible | The acceptance limit focuses only on front-panel color |
The electroplating versus powder coating comparison often starts with appearance, but the more useful split is service geometry. Electroplating introduces metal deposition and surface preparation, while powder coating creates a cured polymer layer. Their visible results, edge behavior, repair methods, and matching controls should therefore be compared separately for each component rather than as a single label covering the entire lock.
My decision sequence starts with the use condition, moves to the component map, and then compares candidate routes. Evidence completeness is the final gate. If a visual preference remains unsupported by a controlled sample, the correct action is to hold that portion of approval rather than let it disappear into a general product approval.
Entry seven: rebuild the sample at the return desk
Back at the system integrator’s desk, the qualification looked different from the factory sample meeting. An illustrative retrofit scenario involved an existing timber door, a metal strike plate, and a reader panel that would remain visible at hand height. The retrofit survey changed the finish decision because the service objective was an appearance match with nearby hardware, not an isolated display-panel match.
In that scenario, the panel sample could pass color review, but the matching plan still lacked a replacement route. The team could describe what it wanted, yet it could not identify who would supply a later panel with the same appearance. The qualification therefore remained open on serviceability even though the finish itself looked acceptable.
A second illustrative scenario involved hotel-room hardware where escutcheon consistency mattered across several door types. The common finish had to coexist with different lock cases, strike plates, handles, and service arrangements. The useful conclusion was to divide the approval by part family instead of applying one sample to a complete room set.
These scenarios are not project reports. They show why the sample record must return with the commercial and technical file. The questions it raises are more useful than a fictional success story: which component fails first, who replaces it, what evidence supports matching, and which requirement remains unverified.
Entry eight: write the quote as a controlled decision
The cost worksheet attached to the qualification should mirror the part map. Process, color, part family, geometry, masking, inspection, packaging, spare quantity, and MOQ assumptions belong on separate lines. That structure exposes differences hidden inside a single product quotation.
I would ask for exact figures through the request-a-quote page after the finish scope has stabilized. The sample order page can establish which controlled pieces are needed for approval, while the catalog request page can support the broader product and documentation review. These steps keep the finish decision tied to an identifiable configuration rather than an attractive but undefined sample.
The commercial review should also show what happens when the requirement changes. A new color, mixed substrate, additional masking, different visible side, or higher matching burden may alter the route. The quote should identify the assumptions that can be changed without recreating the process and the decisions that require a new sample and renewed review.
The approval sheet I would actually send
Before release, I would send a short, traceable approval sheet rather than a general statement that the finish is acceptable. It would contain the following items:
- Visible, contact, concealed, and moving parts identified separately.
- One controlled approval sample linked to the drawing revision.
- Substrate and finish route stated for each relevant component.
- Masking and exposed-area boundaries recorded.
- Cosmetic limits connected to actual receiving inspection conditions.
- Test evidence indexed against the project’s wear and environmental questions.
- Service replacement, matching, and master-sample responsibilities assigned.
- Quote assumptions aligned with the approved part and color scope.
- Change-notification and corrective-action routes defined.
- Unresolved evidence listed rather than hidden inside a blanket approval.
CONFIRM-WITH-LOCAL-QUALIFICATION-TEAM: Verify any project-specific access-control, building, coating, or environmental requirements with the relevant local authority and the dated product evidence before release.
Appearance approval, durability evidence, and service feasibility do not need to pass on the same day. Recording them separately prevents a strong showroom sample from carrying a weak service method into production. It also gives the factory a precise response path when a finish, part, or process assumption changes.
The surface finish processes tradeoffs I carried home
The notebook’s final conclusion was not that one process was best. It was that the buyer had to decide which promise mattered most for each part and which evidence would support it. A controlled sample established appearance; the part map connected appearance to function; the quote exposed the assumptions behind cost; and the service exercise showed whether the finish could survive ownership.
The practical counterpart to this point is how to source smart locks from china. That is the same question surface finish processes tradeoffs has to answer here.For a system integrator ready to turn this qualification into a controlled sample request, the practical next step is to send the part map, finish requirements, evidence questions, and unresolved risks together through the request-a-quote page. That keeps the commercial discussion anchored to the same configuration the factory is being asked to evaluate.